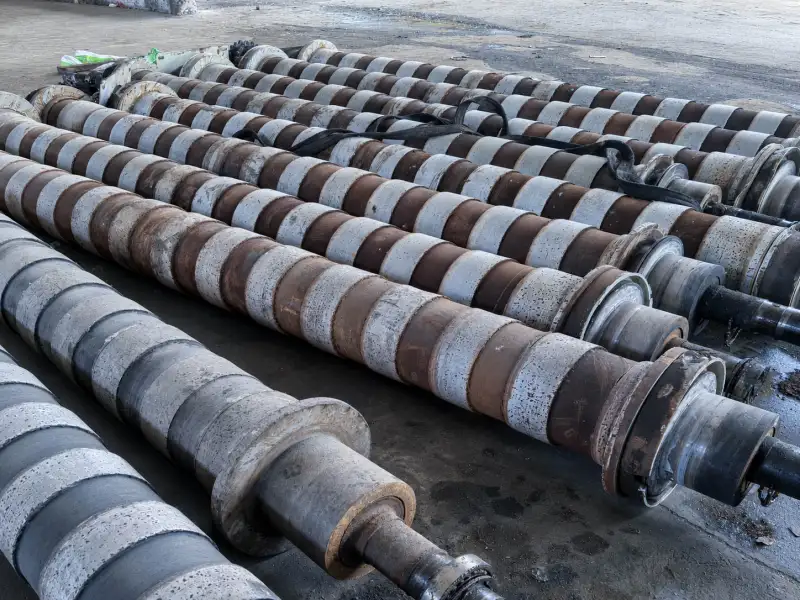
What Each Location Tells You
Across the Full Working Face
Similar change across most of the working face points to broad exposure.
The roller may receive continuous spray, partial immersion, acid carried by the strip, or repeated wetting during production. Cleaning liquid and rinse water belong in the same record. They may touch the cover at a different temperature or remain on the surface longer than the process acid.
A roller left wet during shutdown also sees a different contact cycle from one that is rinsed and dried soon after production.
Check whether:
- the changed area follows the normal wet zone;
- the roller diameter has increased across the full face;
- the center and edges feel equally soft or hard;
- the surface remains changed after drying;
- the failure appeared faster after a change in acid, cleaner, rinsing, or shutdown practice.
Broad swelling or surface change brings the rubber material into the review. General cracking, swelling, softening, and hardening are covered in more detail in Rubber Roller Failure Signs.
Along the Working-Face Edge
The working-face edge is the outer band of the rubber surface. It is separate from the roller end face.
The moving strip may wipe liquid from the center while the outer band stays wet. On squeeze positions, liquid can also move sideways through the contact area and collect near the end of the rubber cover.
Compare both edges and measure the width of the damaged band.
Damage on one side often follows strip tracking, spray direction, machine slope, or uneven drainage. Similar damage on both sides points toward the repeated cover-ending detail or liquid collecting outside the normal strip path.
Common signs include:
- a raised or enlarged edge band;
- rubber that feels softer or stickier than the center;
- a circular crack close to the cover edge;
- staining around the cover ending;
- lifting that starts at the outer edge;
- damage aligned with the normal strip edge.
For wet squeeze positions, the Squeeze and Dewatering Rollers page covers the roller requirements around liquid removal and wet contact.
At the Roller End
The roller end includes the area beside the working face where the rubber cover finishes.
Splash, overflow, washdown, and liquid running along the roller can reach this area. Rotation may carry some liquid away during production. After shutdown, residue can remain against the same cover boundary for hours.
End-entry failures often develop in this order:
- staining, softening, or swelling appears near the end;
- a crack or small opening forms around the cover ending;
- liquid moves beneath the rubber;
- rust or local lifting appears farther inward.
Repeated failure on the same machine side is useful evidence. Photograph the nearby spray direction, drainage route, exposed steel, and any damage caused during cleaning or maintenance.
The next roller should address the end detail as well as the rubber material. A stronger compound cannot close an open path at the cover edge.
Around Segment Gaps
Every segment gap creates two rubber side faces and a narrow space where liquid, scale, or cleaning residue can remain.
The gap may open slightly while the roller is loaded. When the load is released, it can close around retained liquid or debris. Repeated movement damages the same edge and gives liquid more access to the segment side.
Inspect every gap, not just the worst one.
A single failed gap usually points toward local damage, poor assembly, trapped scale, or movement of one segment. Similar damage at most gaps points toward the repeated segment detail.
Record:
- which gaps are affected;
- whether the damage continues around the full circumference;
- gap width at several positions;
- the condition of the segment sides;
- scale or hard debris inside the gap;
- loose or moving segments;
- repair or re-covering history.
A change from segmented to continuous covering can affect the roller’s original function and maintenance method. Any construction change should start from the roller position and the reason the segmented design was used.
Under the Rubber Cover
Local lifting or cover separation shows that the failure has reached the rubber-to-steel area.
Liquid can enter through an end opening, segment gap, deep crack, cut, or damaged cover edge. Once it reaches the steel, corrosion can spread under rubber that still looks intact from the outside.
Typical signs include:
- rust staining at the cover edge;
- a local bulge;
- a hollow response when the surface is tapped;
- lifting beside a crack or segment gap;
- separation growing inward from one end.
After stripping the old cover, inspect the steel directly below the first damaged location. Photograph corrosion, pitting, previous welds, repaired areas, remaining adhesive, and any loss of the original core shape.
Deep corrosion can make the old core unsuitable for another covering cycle. The decision should be made after the damaged area is exposed and measured.