
Защитные чехлы для рулонов пленочного ламинирования печатных плат: проверка возможности замены.
A PCB dry film laminator rubber roller needs replacement, but the purchase request may only specify a “heated laminating roll.” The first step is to identify the actual part: the rubber cover, a removable outer cylinder, or the complete heated assembly.
If the original roller worked well and operating conditions have not changed, its drawings and specifications provide a practical starting point. A worn cover may be re-covered if the metal core is suitable for reuse. A complete new rubber-covered roller can also be ordered from confirmed drawings or a suitable sample.
An integrated heated assembly requires closer confirmation because the roller body, heaters, sensors, and electrical connections may involve separate manufacturing responsibilities.
If you do not have the complete drawing, photos of the old roller and its OEM part number are enough to start identifying the replacement.
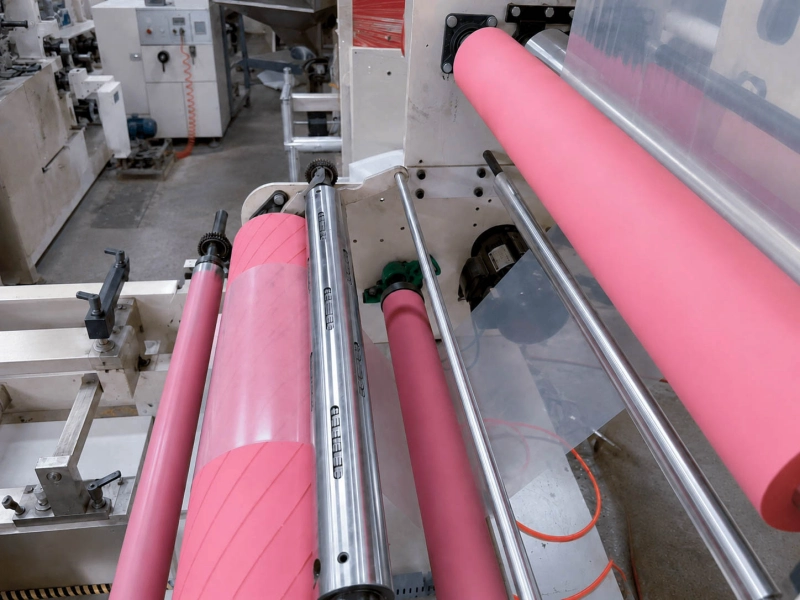
Identify the Part You Are Replacing
A heated laminating roll can have different constructions. Some use a conventional rubber-covered metal body. Others may have a removable outer cylinder or heating components integrated into the roller assembly.
The replacement scope follows the actual construction.
When only the rubber is worn, inspect the existing core. Damage to the metal body, mounting areas, or bonding surface may make a new roller preferable to re-covering.
A removable cylinder needs its own dimensional and structural information. Its internal fit and connection details matter because the replacement must assemble correctly with the parts being retained.
For a complete heated assembly, the OEM drawing should identify the mechanical roller and associated heating components separately. The machine model or part number alone cannot establish the internal construction.
What Can Be Quoted From the Existing Information?
| Re-cover to drawing | Construction needs confirmation | Separate scope confirmation required |
|---|---|---|
| The rubber cover needs replacement, and the existing core is identified and suitable for reuse. | The required part is a removable cylinder, or the internal heating arrangement is unclear. | The request includes a complete heated assembly, electrical components, safety parts, or guaranteed OEM compatibility. |
| Confirm the original cover specification and core condition, then proceed with the re-covering quotation. | Obtain the assembly drawing or sample. Identify the cylinder, mounting interfaces, and parts being retained. | Confirm the technical documents, order scope, and manufacturing responsibility before including these items in a quotation. |
A complete new rubber-covered roller can also proceed directly to quotation when its mechanical drawings and specifications are clear.
Keep the Original Fit and Heating Path
A replacement roll must fit the existing laminator. Start with the OEM drawing and check the finished outside diameter, rubber face length, shaft ends, bearing seats, and mounting interfaces.
Pay attention to how dimensions are recorded. The metal core diameter and finished roller diameter are different measurements. Rubber face length and overall shaft length are different as well. Confusing either pair can produce a roller that meets the supplied dimensions but cannot be installed correctly.
If the roller contains heating components, the drawing should also show any relevant internal passages, end connections, or sensor locations. These details determine which parts can remain in the machine and which features the replacement must accommodate.
Why Cover Thickness Matters
Where heat is supplied through the roller body, it passes through the rubber cover before reaching the contact surface.
Two rollers can have the same finished outside diameter but different core diameters and cover thicknesses. They may fit the same mounting space while behaving differently under heat and pressure.
For example, increasing the cover thickness while reducing the core diameter can preserve the finished outside diameter. However, the thicker rubber layer changes the heat-transfer path and how the cover deforms under load. Matching the outside diameter alone is therefore insufficient for this type of redesign.
The original cover thickness, rubber specification, and bonding construction should remain the starting point for a proven replacement.
Temperature records also need a clear reference. A heater setting, roller surface temperature, and panel temperature describe different conditions. Identify which one appears in the OEM specification and retain the applicable requirement.
The machine’s loading arrangement affects contact across the PCB width. A documented end-loaded heated-roll design, for example, shows reduced pressure and heat transfer toward the panel center. That behavior is specific to the construction and cannot be assumed for every laminator.
For a straightforward replacement, preserve the original roller geometry and heating-related specifications. Changes to the cover construction need confirmation against the actual machine requirements.
Волорина Прижимные валы page provides further information on rubber-covered rollers used for controlled nip contact.
Check the Surface That Contacts the Dry Film
Dry-film lamination requires a clean roller surface and consistent contact. A new cover should reproduce the surface condition that worked on the original roller.
First, confirm which side of the material touches the rubber. Depending on the film path and laminator design, the roller may contact the carrier film rather than exposed photoresist or copper.
This matters when specifying the surface finish. A texture suitable for one contact arrangement should not automatically be copied to a different one.
Look closely at the old cover. Embedded particles, cuts, hardened deposits, or persistent residue can interfere with contact. If the original finish worked well before the cover deteriorated, reproduce that finish rather than introducing a different texture without a clear reason.
Check the Bond Before Re-covering
The rubber-to-core bond deserves particular attention on heated rolls.
If the cover is lifting at the ends or separating from the metal, inspect the core surface and the failed bonding area before deciding to reuse the core.
Also confirm the actual temperature exposure and cleaning liquid when they differ from the original conditions. A replacement compound should be selected against those conditions rather than copied solely from the old material name.
Contamination from incoming film, handling, or another machine component needs to be addressed at its source. Roller replacement is relevant when the rubber surface or cover condition is contributing to the contact problem.
When the Original Hardness and Profile Need a Second Look
The original hardness record is usually more useful than a measurement taken from a worn, heat-aged cover.
Rubber can harden or soften during service. If the old cover has been exposed to heat for years, its current hardness may no longer represent the original specification. Use the OEM drawing or earlier acceptance record where available.
Check the finished roller profile as well. The drawing may specify a straight face, a crown, or particular runout and dimensional tolerances. These details affect how the roller fits and contacts the material.
A roller with a good service history can normally be replaced to its original specification when operating conditions remain unchanged.
Repeated cover failure or a change in working conditions calls for a closer look.
For example, if the operating temperature has increased and the old cover now cracks or loses adhesion, check the rubber compound and bonding construction against the new exposure before repeating the original build.
If the cover remains sound but lamination results differ across the panel width, confirm the machine’s loading arrangement and roller mounting condition before changing the rubber hardness or profile.
Changes to hardness, cover thickness, or crown should be based on an identified requirement. The original drawing remains the reference for dimensions and tolerances until a revised specification has been confirmed.
What Information Is Needed for a Replacement Quote?
For a standard replacement, an OEM drawing or confirmed roller specification is usually sufficient to start a quotation.
The drawing should identify the required part, finished dimensions, mounting details, and rubber-cover specification. Include the drawing revision or OEM part number when available, particularly if the machine has undergone previous modifications.
Be careful with dimensions measured from a worn cover. Its current diameter may be smaller than the specified finished diameter. Use the original drawing to establish the replacement size where possible.
For a heated roller, provide the relevant temperature requirement and available assembly information. If the drawing does not clearly separate the roller body from its heating components, a sectional drawing or photographs of the removed part can help clarify the construction.
When the original specification is no longer suitable, include the changed working conditions and the old cover’s failure signs. This helps narrow the rubber and construction requirements before manufacturing.
A complete drawing is not required for an initial discussion. The known roller dimensions, its position in the laminator, and photographs of the old part can establish where to begin.
Связанные страницы
Rubber-covered pressure rollers for controlled nip contact and application-specific replacement.
Валы для линий нанесения покрытий и ламинирования
Roller requirements for coating and laminating applications, including heated contact and surface protection.
Для получения точной цены на ролик, пожалуйста, пришлите ваши чертежи или подтвержденные размеры, необходимую деталь и детали крепления. Если информация неполная, предоставьте старые фотографии ролика, его положение, материал контакта и текущую проблему, связанную с роликом.