Feeding stability
Slip, short infeed inconsistency, and handover repeatability

Los rodillos de presión se utilizan cuando es necesario sujetar, alimentar y guiar materiales a través de un punto de contacto controlado.
They usually work together with another roller to form a controlled nip contact, helping film, paper, label stock, packaging film, printed substrates, and other web materials enter the next section of the line more steadily.
In production, the main role of a pinch roller is to hold the material at the right contact point, feed it into or through the station, and keep it moving in sync while reducing the risk of slipping, indentation, tracking disturbance, or surface marks.
If you already have an existing roller size, drawing, sample, or roller specification, you can send it to us directly.
If the material, hardness, or surface is not yet confirmed, we can also start from the roller position and the problem you are trying to solve.
A pinch roller, also called a nip roller or pinch feed roller, provides controlled holding and feeding contact when material enters, passes through, or exits a machine section.
Los puestos más comunes incluyen:
Infeed and outfeed sections
Before or after printing, coating, or laminating stations
Around slitting and rewinding sections
Label, film, paper, and flexible packaging web paths
Short-distance feeding points where stable holding contact is required
A pinch roller may not be the most visible roller in the line, but it can directly affect how stable the material is before it reaches a key process section.
When the pinch contact is unstable, the line may show slipping, uneven feeding, wrinkling, indentation, or web tracking disturbance.
This type of requirement is usually reviewed first as a function page. When the same project is strongly tied to broader web-handling conditions, it may also connect naturally to Rodillos para conversión de película.
The same pinch roller logic does not behave the same way at every station.
The main concern is usually whether the material can be caught steadily before the next section starts to influence it.
Typical concerns:
unstable entry
short slipping during start-up
the web not entering straight
one side feeding earlier than the other
El contacto generalmente debe mantenerse estable, pero también debe ser suave.
Typical concerns:
entry instability affecting downstream quality
local marks on sensitive surfaces
widthwise pressure difference
feeding mismatch before the next section
This position often needs stronger feeding control, but pressure cannot simply be increased without consequences.
Typical concerns:
slip after speed increase
narrow materials running less steadily than before
marking on thin or soft substrates
unstable handover before winding
These positions usually depend more on repeatable grip recovery than people expect.
Typical concerns:
local slip during restart
inconsistent feeding length
repeated marking at the same contact point
unstable catch after repeated cycles
Increasing pressure is not always the right answer, because too much pressure can create indentation or material deformation.
If the main symptom is surface damage, pressure distribution, surface roughness, and contact uniformity should be checked together.
If the pinch roller does not stabilize the material before the next section, printing, coating, laminating, slitting, or rewinding may also be affected.
This type of problem should be checked together with downstream traction, tension, and web guiding conditions.
In this situation, the material alone is not enough to judge the problem. Mechanical alignment and contact uniformity also need to be reviewed.
A pinch roller usually needs to control four things at the same time:
Slip, short infeed inconsistency, and handover repeatability
Marks, indentation, stretching, and surface damage
Grip, release, contamination tendency, and material protection
One-side tightness, local pressure difference, and uneven catch across the face
A good pinch roller is not the one with the highest pressure. It is the one that provides enough holding force while keeping the contact stable and manageable for the material.
Los rodillos de presión suelen necesitar un equilibrio entre agarre, deformación y protección de la superficie.
For many industrial pinch / nip contact positions, rubber cover hardness is commonly selected within the range of 40–90 Shore A.
| Application Goal | Common Hardness Direction |
|---|---|
| Softer holding contact and lower marking risk | Around 40–60 Shore A |
| General feeding for packaging, printing, labels, or web materials | Around 60–80 Shore A |
| Higher grip, higher wear, or heavier contact load | Around 80–95 Shore A |
| Heat, release, or anti-stick contact | Depends on compound and surface treatment |
Around 40–60 Shore A
Around 60–80 Shore A
Around 80–95 Shore A
Depends on compound and surface treatment
These ranges are only starting points.
The same Shore A hardness can behave differently depending on nip pressure, cover thickness, roller diameter, line speed, and the material surface.
When designing or replacing a pinch roller, the following points usually need to be checked together:
Copying the old roller is usually enough when the previous contact ran steadily and the line conditions have not changed.
If line speed, substrate surface, material thickness, tension setting, or mating roller condition has changed, the old specification should be treated as a reference, not the final answer.
In these cases, the roller size can still be used as a starting point, but the material, hardness, surface finish, and contact condition should be checked again before production.
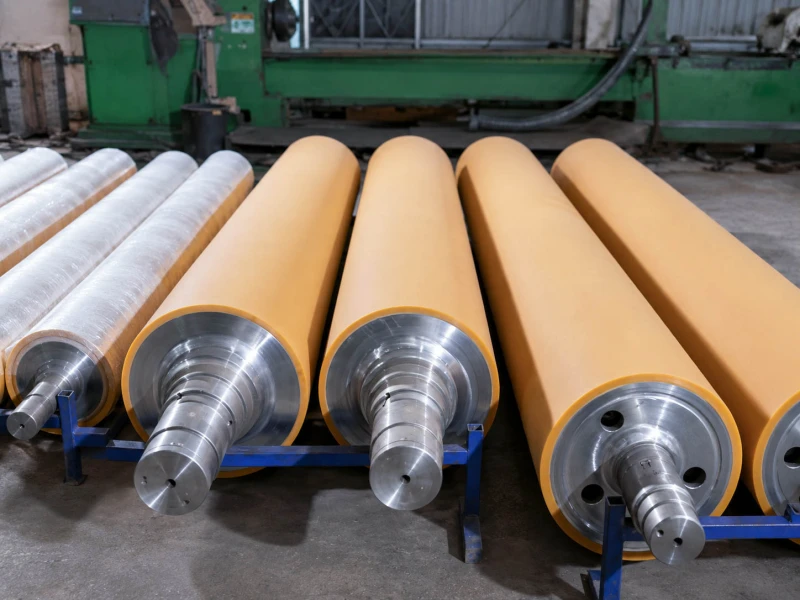
Material selection should start from the station requirement, not from habit alone.
rodillos de caucho de poliuretano are often reviewed first where stronger traction feel, cut resistance, and longer wear life are important.
Rodillos de caucho NBR/nitrilo are often reviewed where oil, ink, adhesive-related exposure, or general industrial feeding conditions are involved.
rodillos de silicona sólida are often reviewed where release behavior, heat resistance, or lower surface aggression becomes more important than maximum traction.
EPDM may be reviewed where moisture, ozone, or more open-environment exposure matters more.
FKM, HNBR, CSM, butyl, or other compounds may need to be reviewed from the actual operating condition rather than from a default material habit.
El material sigue siendo solo una parte de la decisión. En los rodillos de presión, la dureza, el acabado superficial, el espesor de la cubierta, el estado de los rodillos emparejados y el comportamiento real de la estación a menudo influyen en el resultado de la misma manera.
Not every feeding problem should be judged as a pinch roller problem first.
The issue starts at a short local holding point
The material enters the next section unstably
Slip appears exactly at the nip point
Marks appear where the paired contact is applied
The material is being caught, handed over, or restarted poorly
The main problem is continuous pulling and speed synchronization → rodillos de tracción
The main problem is wider pressure distribution or surface protection across a broader contact zone → rodillos de presión
The pinch point is only the visible symptom and the real instability starts elsewhere on the line
The position is part of a broader thin-web handling process that also needs application-level review → Rodillos para conversión de película
Replacing a pinch roller alone will not fully solve a line problem that is actually traction-related, pressure-distribution-related, or broader than the local contact point.
Slipping may be related to surface friction, hardness, nip pressure, material surface condition, or speed synchronization.
Increasing pressure is not always the right answer, because too much pressure can create indentation or material deformation.
These problems may come from unsuitable hardness, excessive pressure, rough roller surface, local pressure variation, or a sensitive material surface.
If the main symptom is surface damage, pressure distribution, surface roughness, and contact uniformity should be checked together.
If the pinch roller does not stabilize the material before the next section, printing, coating, laminating, slitting, or rewinding may also be affected.
This type of problem should be checked together with downstream traction, tension, and web guiding conditions.
This may be related to roller parallelism, mounting pressure, cover condition, crown profile, or roller accuracy.
In this situation, the material alone is not enough to judge the problem. Mechanical alignment and contact uniformity also need to be reviewed.
Often reviewed when stronger grip, toughness, and wear resistance are needed.
Rodillos de caucho NBR / nitriloOften reviewed for general industrial feeding, oil, ink, or adhesive-related contact.
Rodillos de silicona sólidaOften reviewed when gentler contact or lower marking tendency matters more.
Rodillos de presiónUseful when the main question is wider pressure distribution rather than local pinch holding.
Rodillos de tracciónUseful when the line problem is more about continuous pulling and speed synchronization.
Rodillos para conversión de películaUseful when the pinch point is part of a broader thin-web handling process.
Rodillos para embalaje flexibleUseful when printing, laminating, feeding, and rewinding influence each other on the same line.
Rodillos para líneas de corte longitudinal y rebobinadoUseful when the main issue appears at slitting entry or rewinding handover.
Un rodillo de caucho fiable depende de algo más que la coincidencia dimensional. La formulación del compuesto, la estabilidad de dureza, el espesor del recubrimiento, el acabado superficial, la estructura del eje y la precisión de giro influyen en su comportamiento en la línea.
Wolorin trabaja tanto en sustituciones rutinarias como en proyectos industriales de rodillos de caucho a medida más exigentes, con experiencia de fabricación, equipos de producción e inspección, certificaciones disponibles y controles de calidad documentados. Nuestro sistema de formulación de compuestos puede adaptarse a diferentes requisitos de operación.
Antes del envío pueden comprobarse, según el proyecto, elementos clave como dureza del recubrimiento, detalles del eje, estado superficial y precisión de giro.
Puede consultar nuestro ámbito de fabricación, el proceso de control de calidad y los antecedentes de la empresa en las páginas que aparecen a continuación.
Wolorin puede fabricar rodillos de presión a medida basándose en las dimensiones, planos, muestras o requisitos específicos de su estación de trabajo.
If the current roller slips, leaves marks, or feeds unstably, you can send us the roller details or application information so we can help confirm the material, hardness, surface, and replacement direction.