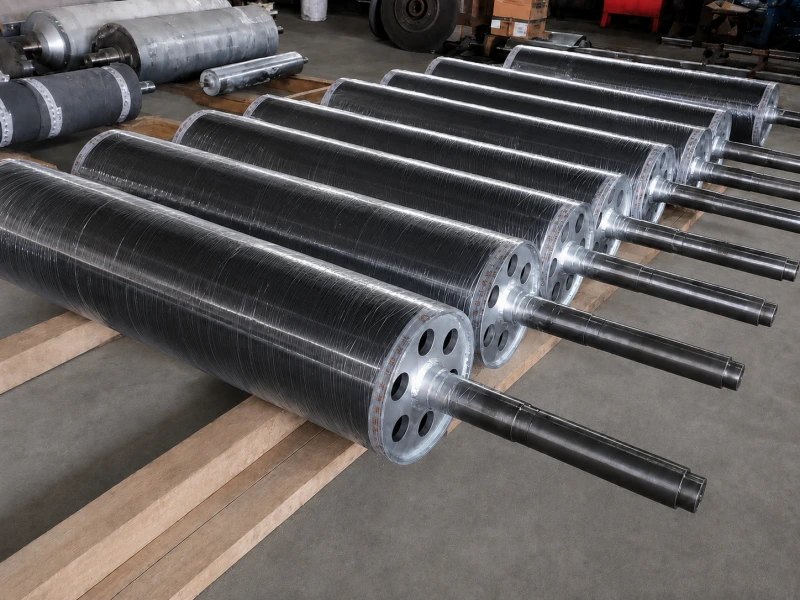
Oily Strip Needs a Surface That Can Manage the Oil
Main priority: Stable traction through the oil film and a surface that remains cleanable.
Where the trade-off sits: Texture and grooves can move oil away from the contact, but they can also hold oil, fines, and cleaning residue.
Confirm before specifying: Oil type, approximate amount, distribution across the strip, cleaning liquid, cleaning method, strip width, surface requirement, and how quickly slip returns after cleaning.
Oil creates a separating layer between the steel and the cover. A compound with good dry friction can still slip when oil remains inside the working contact.
A light, even oil film may need only a fine, controlled texture. Heavier or uneven carryover may require a more open finish or a drainage groove. Groove direction should follow the actual strip path, roll rotation, and the direction in which liquid can leave the contact. A standard groove copied from another line can push oil toward the strip edge or create pockets that are difficult to clean.
The time between cleaning and renewed slip is useful evidence. If cleaning restores grip and the problem returns after several production cycles, the surface is probably rebuilding a layer of oil, metal fines, and residue. A harder or more wear-resistant compound does not remove that layer.
A very soft cover may give better short-term traction because it conforms more closely around the oil film. Under continuous load, it can run hotter, spread contaminated oil across the face, and suffer deeper edge cuts.
Rodillos de caucho NBR/nitrilo are often considered for oil-contact positions. The process oil, cleaning liquid, temperature, load, surface requirement, and old-roll condition still decide whether the specific rubber direction is suitable. Polyurethane can also be relevant where abrasion and edge cutting are severe, provided its behavior in the actual oil and cleaning environment is appropriate.
Wet and Chemical Contact Can Affect More Than the Surface
Main priority: Compound stability, protection of the bonding interface, drainage, and working-diameter stability.
Where the trade-off sits: A surface that drains well during running may hold residue when the roll stops wet.
Confirm before specifying: Exact contact liquid, exposure pattern, cleaning medium, temperature, wet shutdown condition, visible cover change, edge damage, and measured diameter change.
“Wet strip” covers several different conditions. Rinse water, alkaline cleaner, acidic carryover, degreasing liquid, and metal-treatment chemicals do not affect a rubber cover in the same way.
The first concern is whether the cover changes after repeated exposure. Swelling increases the effective diameter and usually changes the surface feel. Softening can increase deformation and edge cutting. Hardening reduces conformity and may increase strip marks. Cracks and damaged edges give liquid a route toward the bonding interface.
Shutdown conditions matter. A groove can drain well while the line is moving, yet retain liquid when the roll stops wet. Residue can collect in the groove or inside an edge cut. Damage may begin in one small area while the rest of the face still appears usable.
A chemically suitable compound can still fail when the cover end, edge construction, bonding, or core preparation is weak. For this type of roller, the rubber system and rubber-to-core construction need to work together.
The useful project information is specific: the liquid touching the cover, the cleaning medium, the roller position, old-roll photos, visible surface changes, and measured diameter differences. Chemical concentration, treatment settings, and wider process adjustments remain with the customer’s process team.
For wider metal-treatment applications, see Rodillos de caucho para acero y metalurgia.